
지식
프리폼 선반 척 부품: 맞춤형 가공 및 공작물 고정 점검
10월
Preform Lathe Chuck Components는 정밀 워크홀딩이 고온 증착과 만나는 지점에 위치합니다. OVD, VAD 또는 MCVD 공정을 운영하는 엔지니어에게 척은 단순한 장착 장치가 아니라, 버너, 토치 또는 트래버스 시스템이 공정 전반에 걸쳐 기준으로 삼는 회전 축을 확립하는 요소입니다. 척 조가 마모되거나, 안착면이 열화되거나, 교체용 조 세트가 완전한 치수 데이터 없이 가공되면, 그로 인한 런아웃은 누구도 워크홀딩을 의심하기 훨씬 전에 그을음 증착 비대칭, 테이퍼 변동 또는 일관되지 않은 굴절률 프로파일로 나타납니다.
이 글에서는 Preform Lathe Chuck Components에서 무엇을 검사해야 하는지, 주문 전에 커스텀 preform chuck 부품을 어떻게 평가해야 하는지, 그리고 원래 설계 의도에 부합하는 교체용 워크홀딩을 제작하기 위해 기계 가공 업체에 어떤 정보가 필요한지 다룹니다.
Preform Lathe Chuck Components의 실제 역할
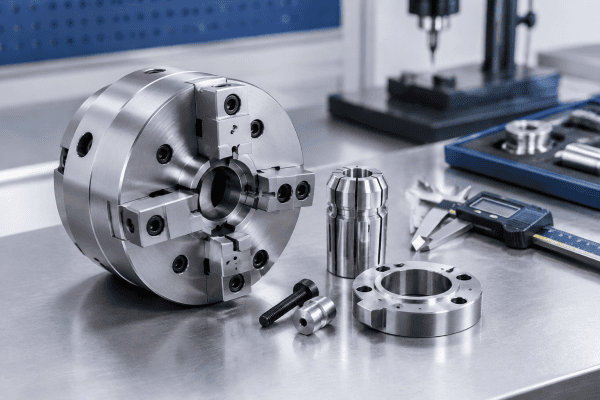
Preform lathe는 버너가 그을음을 증착하거나 preform이 용융 및 연신되는 동안 glass bait rod, target rod 또는 starting tube를 고정합니다. 척은 — three-jaw scroll, collet-style closer 또는 커스텀 split-clamp 설계이든 — 동시에 세 가지를 수행해야 합니다:
- 작동 회전 속도에서 미끄러짐 없이 토크를 전달할 것
- 증착 공정에서 요구하는 공차 내에서 반경 방향 런아웃을 유지할 것
- preform 간 변동이 통제된 상태로 유지될 만큼 클램핑 위치를 반복 정밀하게 재현할 것
이러한 기능들은 상호 의존적입니다. 확실하게 파지하지만 축 방향 기울기를 유발하는 척은 휘어진 preform 축을 만들어냅니다. 런아웃은 우수하지만 클램핑력이 불충분한 척은 가속 중 미세 미끄러짐을 허용할 수 있으며, 이는 표면 자국이나 국부적 직경 변동으로 나타납니다.
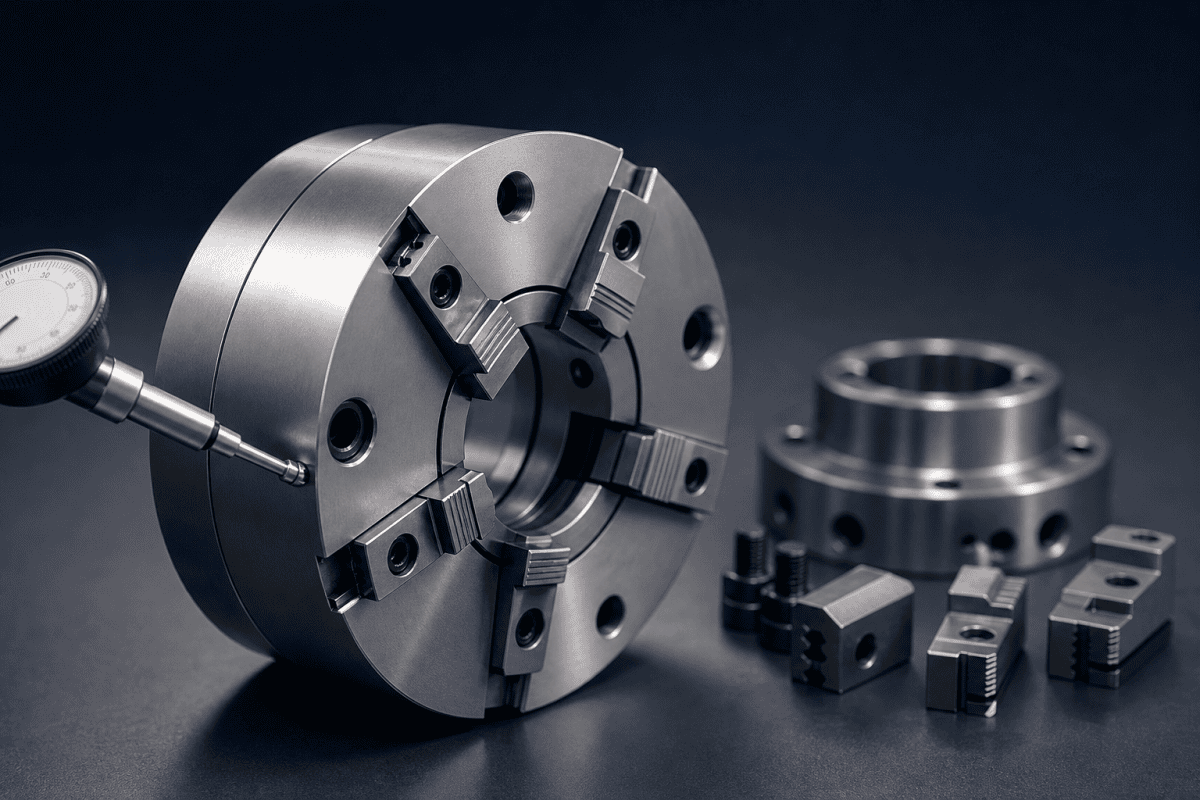
관련된 컴포넌트는 일반적으로 조 인서트 또는 접촉 패드, 조 캐리어, 스크롤 플레이트 또는 클램핑 링, 백플레이트, 어댑터 플레이트, 그리고 때로는 척을 선반 스핀들에 위치시키는 커스텀 스페이서 또는 정렬 피처를 포함합니다. 이들 각각은 독립적으로 마모, 변형 또는 손상될 수 있습니다. 이러한 preform lathe chuck components의 전반적인 상태가 증착 공정의 반복 정밀도를 결정합니다.
정밀 워크홀딩 컴포넌트의 검사 항목
교체품을 주문하기 전에 실제로 문제를 일으키는 컴포넌트가 무엇인지 파악하는 것이 도움이 됩니다. 접촉 패드만 마모된 경우 전체 척 어셈블리를 교체하는 것은 비용이 많이 들고 불필요합니다. 반대로 변형된 스크롤 플레이트를 위해 새 조를 가공해도 동심도는 회복되지 않습니다.
조 접촉면 및 인서트
유리 또는 캐리어 로드에 접촉하는 조 인서트는 가장 흔한 마모 품목입니다. 다음을 확인하십시오:
- 접촉 패턴: 조 면을 따라 균일하고 전체 폭에 걸친 접촉 자국은 균등한 하중을 시사합니다. 한쪽 끝에 집중된 자국은 각도 오정렬 또는 휘어진 조를 나타냅니다.
- 매립 입자: 연질 조 재질에 눌러진 유리 칩, 그을음 또는 연마성 이물질은 로드를 긁고 그립 일관성을 저하시킬 수 있습니다.
- 변형: 과도한 조임 또는 열 노출은 조 면을 벨형 또는 버섯형으로 변형시켜 유효 접촉 면적을 감소시킬 수 있습니다.
- 재질 상태: 인서트는 용도에 따라 알루미늄, 청동, 폴리머 복합재 또는 기타 재질로 가공될 수 있습니다. 재질 선택은 접촉 압력, 척에서의 온도, 오염 위험, 그리고 유리를 손상시키지 않기 위해 인서트가 약간 변형되어야 하는지 여부에 기초해야 합니다. 알루미늄은 더 가벼운 접촉이나 열전도성이 도움이 되는 곳에 때때로 사용되지만, 모든 척 위치에 적합하다고 가정해서는 안 됩니다 — 알루미늄 컴포넌트가 일반적으로 적용되는 위치에 대한 맥락은 aluminum OVD parts를 참조하십시오.
스크롤 플레이트, 클램핑 링 및 작동면
Scroll chuck은 모든 조를 동시에 움직이는 나선형 플레이트에 의존합니다. 스크롤 치아의 마모는 불균등한 조 전진을 초래하며, 이는 조가 균일하게 닫히는 것처럼 보여도 로드가 중심에 있지 않다는 것을 의미합니다. 다음을 확인하십시오:
- 스크롤 나선의 가시적 마모 또는 갈링
- 조 방향을 반전할 때의 백래시
- 알려진 원형 게이지에 클로징할 때의 조 간 위치 변동
Collet-style 또는 split-clamp 척에서는 클로징 테이퍼와 플렉스 영역에 균열, 영구 변형 또는 불균일한 접촉이 있는지 검사하십시오.
백플레이트 및 스핀들 인터페이스
척을 선반 스핀들에 장착하는 백플레이트 또는 어댑터가 기준 평면을 확립합니다. 이 인터페이스의 먼지, 버 또는 프레팅 부식은 전체 척을 기울게 할 수 있습니다. 백플레이트에서의 작은 각도 오차조차 긴 preform의 먼 쪽 끝에서 증폭됩니다.
장착면의 평탄도, 레지스터 직경의 끼워맞춤, 볼트 구멍의 신장 또는 나사 손상을 확인하십시오. 커스텀 척에서는 레지스터가 스핀들 노즈에 무리 없이 그리고 감지 가능한 유격 없이 끼워맞춤되는지 검증하십시오.
런아웃 측정
반경 방향 런아웃은 척을 장착하고 생산 시와 동일하게 작동시킨 상태에서 측정해야 합니다. 알려진 원통면 — 테스트 바 또는 연삭된 게이지 — 에 다이얼 인디케이터를 사용하여 척 면과 preform의 작업 위치를 나타내는 거리 양쪽에서 측정하십시오. 여러 회전 위치에서 런아웃을 기록하십시오. 런아웃이 회전 각도가 아닌 조 위치에 따라 변하면 문제는 조 또는 스크롤에 있습니다. 회전당 한 번 반복되면 문제는 스핀들, 백플레이트 또는 척 본체에 있을 수 있습니다.
척 이외의 워크홀딩 인터페이스 점검
척은 워크홀딩 인터페이스의 한 요소에 불과합니다. 심압대, 방진구, 그리고 모든 중간 지지대 또한 프리폼 축에 영향을 미칩니다. 척이 센터링되어 있더라도 심압대가 오프셋되어 있으면 프리폼이 휘어집니다. 심압대 센터 런아웃, 방진구 패드 상태, 그리고 전체 이동 범위에 걸친 주축대와 심압대 사이의 정렬을 점검하십시오. 이동되거나 재수평 조정된 선반의 경우, 척을 문제 삼기 전에 이 정렬을 다시 검증해야 합니다.
콜릿 스타일 척의 경우 스핀들 테이퍼와 드로우바 상태도 중요합니다. 마모된 테이퍼나 늘어난 드로우바는 클램핑력을 감소시키고 콜릿이 축에서 벗어나 안착되도록 할 수 있습니다. 드로우바 신장량을 측정하고 테이퍼에 스코어링이나 프레팅이 있는지 확인하십시오.
증착 토치 정렬을 다루는 엔지니어에게 워크홀딩 인터페이스는 더 큰 정렬 체인의 일부입니다. 광섬유 프리폼 장비 및 증착 토치 부품 에 관한 문서는 척 작업과 함께 자주 제기되는 관련 기술 및 소싱 질문을 다룹니다.
커스텀 Preform Chuck 부품을 가공해야 하는 시점
원래 부품을 더 이상 구할 수 없거나, 특정 선반 또는 프리폼 크기에 맞게 척이 개조되었거나, 기존 설계가 사용 환경에서 견디지 못할 때 커스텀 프리폼 척 부품이 필요해집니다. 또한 생산 팀이 다른 로드 직경에 맞게 접촉 패드 형상을 변경하거나 유리에 생기는 마킹을 줄이려 할 때도 커스텀 가공이 일반적입니다.
일반적인 커스텀 부품은 다음과 같습니다:
- Replacement jaw inserts with modified contact geometry or material
- Adapter plates for mounting a chuck on a different spindle interface
- Split-clamp halves machined to a specific preform diameter
- Spacer rings and alignment sleeves that set axial position
- Non-standard backplates where the original is damaged or unavailable
For any of these, OEM/ODM machining services can produce parts from drawings, samples, or measured dimensions. The critical input is not the part name but the functional requirements: what the part must locate, what load it carries, what temperature it sees, and what material is appropriate.
커스텀 척 부품 견적 시 제공해야 할 정보
A machine shop cannot produce a reliable workholding component from a description alone. Useful inputs include:
- Drawings or sketches with critical dimensions, tolerances, and datums. If no drawing exists, provide a physical sample or detailed measurements.
- Material specification or the material of the original part. If the original material is unknown, describe the operating environment — temperature, humidity, contact with glass, cleaning agents — so the shop can recommend a suitable alloy or polymer.
- Interface dimensions: spindle register diameter, bolt circle, jaw slot dimensions, and any keyway or locating feature.
- Operating conditions: rotational speed range, clamping force, rod diameter and weight, and whether the chuck sees radiant heat from the burner or torch.
- Quantity and lead time expectations, recognizing that prototype quantities and production quantities may follow different processes.
- Inspection requirements: which dimensions are critical, and whether a dimensional report is needed.
Photographs of the installed chuck, the worn area, and the spindle interface are often as valuable as a drawing because they show how the part actually fits and wears.
기존 부품으로부터의 역설계
When drawings are unavailable, reverse engineering from a sample is a practical route. Accuracy depends on the condition of the sample and the measurement methods used. A worn jaw insert, for example, may no longer represent the original contact geometry, so the shop must distinguish between intentional features and wear. Hardness testing, material analysis, and careful measurement of unworn reference surfaces help separate design intent from service damage.
For chucks used on SG Controls or similar MCVD lathes, the mounting interface and jaw geometry may be specific to that platform. The guide to SG Controls MCVD lathe spare parts describes typical custom machined holders and carriage components, which provides useful context for how workholding interfaces are documented and reproduced.
If the original chuck design used interchangeable inserts, it may be possible to standardize on a new insert geometry that improves grip or reduces glass marking without modifying the carrier. This kind of incremental change is often more cost-effective than a complete chuck redesign.
교체 전후의 워크홀딩 점검
Installing a new or re-machined chuck component without verification can introduce a new error. A simple sequence helps confirm that the workholding is not the source of process variation:
- Clean all interfaces before assembly. Soot, glass dust, and dried lubricant are common causes of tilt and runout.
- Check register fit by hand. The chuck should seat fully without rocking.
- Torque fasteners evenly in a crossing pattern to avoid distorting the backplate.
- Measure runout at the chuck and at working distance after assembly, using a gauge that represents the preform diameter.
- Clamp a test rod and check for axial tilt by measuring at two points along the rod.
- Run a short deposition or rotation test if the process allows, and compare the result against a known-good baseline.
If runout changes after clamping, the issue may be in the jaw contact or scroll rather than the spindle. If runout is constant but high, the backplate or spindle interface is the more likely source.
Workholding problems sometimes present as deposition problems. If soot deposition becomes asymmetric or the preform develops a taper, the chuck may be contributing. Related diagnostic logic is discussed in the article on refractive index profile drift and burner concentricity, and in the guide to preform end-taper thermal stress, but the chuck should be checked before adjusting burner parameters.
Document the baseline measurements. A simple log of runout at the chuck face and at working distance, recorded after each rebuild, makes it easier to distinguish sudden changes from gradual wear. It also gives the machining team a reference when producing replacement preform lathe chuck components.
척 부품의 재질 및 설계 고려사항
Material selection for precision workholding components depends on the specific function:
- Contact pads and jaw inserts: Must balance grip, wear resistance, and protection of the glass surface. Hard materials resist wear but may mark or chip the rod; softer materials protect the glass but wear faster and may embed debris.
- Structural components (backplates, jaw carriers): Need dimensional stability and adequate stiffness. Thermal expansion mismatch between the chuck and the spindle can change runout as the lathe warms up.
- Components exposed to heat: If the chuck is close to the deposition zone, radiant heating may cause expansion or material degradation. The appropriate material depends on the actual temperature at that location, which should be measured rather than assumed.
Because these requirements vary by lathe, preform size, and process, it is worth reviewing the range of optical fiber equipment parts available as standard items before committing to a fully custom design. In some cases a standard component can be adapted; in others, custom machining is the more reliable route.
Design choices also affect maintainability. Inserts that can be replaced without removing the chuck from the spindle reduce downtime, and clearly defined datums make it easier to verify alignment after service. For lathes that run multiple preform sizes, interchangeable jaw sets or adjustable stops can reduce changeover time while preserving the reference surfaces that keep runout predictable.
Tolerances should match function. Over-tight tolerances on non-critical features increase cost without improving performance, while loose tolerances on locating surfaces directly affect runout. The drawing should identify which dimensions are functional and which are reference only.
Preform Lathe Chuck Components가 더 넓은 증착 공정에 어떻게 부합하는가
The chuck does not operate in isolation. It interacts with the burner traverse, the gas delivery system, and the exhaust flow. Runout in the chuck changes the distance between the burner face and the glass surface, which in turn affects deposition efficiency and soot density. Even a small eccentricity can produce a periodic variation that looks like a burner pulsing problem.
For this reason, maintenance planning should treat the workholding and the deposition torch as a single alignment chain. When a burner is replaced or repositioned, it is worth confirming that the chuck is still centered and that the preform axis has not shifted. Conversely, when a chuck is rebuilt, the burner alignment should be re-checked before the next production run.
Burner components themselves are subject to wear and can introduce their own variation. Sourcing guides such as the Nextrom VAD burner replacement parts guide or the overview of OVD 버너 부품 explain how those consumables are specified and replaced. Keeping both the workholding and the burner in specification reduces the chance of misattributing a deposition defect to the wrong subsystem.
For processes that require precise refractive index profiles, the combination of chuck runout, burner concentricity, and traverse stability determines the final result. Measuring each contribution separately is the only reliable way to isolate a problem when the profile drifts.
자주 묻는 질문
Preform Lathe Chuck Components는 얼마나 자주 검사해야 합니까?
Inspection frequency depends on operating hours, rotational speed, and contamination levels. A practical approach is to check jaw contact patterns and runout at each scheduled maintenance interval, and to inspect immediately after any incident that could have overloaded the chuck — a jam, a crash, or a preform break during rotation. Trending runout measurements over time is more useful than a single check because it reveals gradual wear. Many facilities find that inspecting these preform lathe chuck components at every major maintenance window is sufficient, with additional checks after any abnormal event.
마모된 척 조를 교체 대신 수리할 수 있습니까?
In some cases, jaw inserts can be re-machined or replaced while the jaw carrier is reused. This depends on whether the carrier itself is distorted and whether re-machining would remove too much material or change the clamping geometry. For scroll plates with worn teeth, repair is rarely practical, and replacement is usually more reliable. A machine shop can assess the worn part and advise based on measured condition. When repair is chosen, the resulting preform lathe chuck components should be re-measured to confirm that clamping geometry still meets the original specification.
Preform Lathe Chuck에서 런아웃의 가장 흔한 원인은 무엇입니까?
Contamination or damage at the spindle-to-backplate interface is one of the most frequent causes, followed by uneven jaw wear. Because the interface error is amplified over the length of the preform, a small amount of debris or a burr can produce significant runout at the working position. Cleaning and inspecting this interface is a logical first step before suspecting the chuck body or jaws. If the interface is clean and the runout persists, then the jaws, scroll, or spindle bearings become the next candidates.
OVDParts는 샘플로부터 척 부품을 역설계할 수 있습니까?
Reverse engineering from a physical sample is possible when the sample is complete enough to measure critical features and when the material can be identified or a suitable substitute specified. The more dimensional and functional information provided, the more reliable the result. For components where the sample is worn or incomplete, drawings and interface measurements from the lathe are important supplements. In many cases, a combination of a worn sample and a few key measurements from the machine is enough to produce replacement preform lathe chuck components that restore original performance.
다음 단계
If you are evaluating replacement preform lathe chuck components or planning a custom workholding project, gather the drawings, sample measurements, material details, and operating conditions described above. Sharing these inputs with the manufacturer allows a more accurate assessment of feasibility and cost. To discuss a specific component, contact our team with your dimensions, material requirements, and the operating conditions the part must withstand.
For broader context on preform equipment parts and how they are sourced, the ISO 10110 optical drawing standard provides useful guidance on specifying tolerances for optical components, which can inform how you document critical dimensions on your own drawings.
