Knowledge
Preventing Premature Silica Soot Clogging and Vitrification on OVD Burner Faceplates: Root Causes and Shop Protocols
Sep
During high-rate Outside Vapor Deposition (OVD), few events disrupt target growth faster than premature crust formation on the torch faceplate.
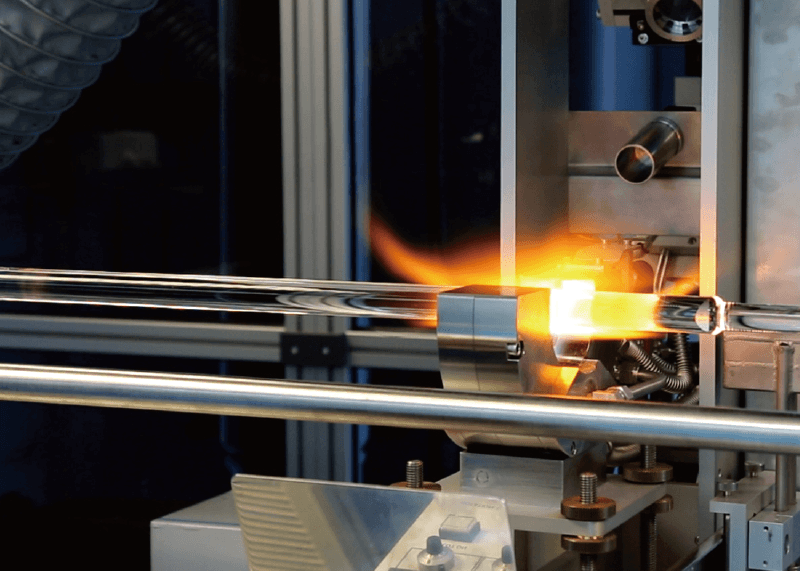
When nascent silicon dioxide (SiO₂) soot clings to the discharge orifices rather than traveling toward the rotating target rod, the high radiant heat of the reaction zone (>1400°C) rapidly sinters those particles into hard, transparent silica glass.
Once this vitrification process begins, gas stream boundaries collapse. Flow velocities become erratic, flame geometry destabilizes, and operators are forced to pause deposition, cool the chamber, and pull the lathe off-line.
Chemical Hydrolysis at Flame Front:
SiCl₄ + 2H₂O ──> SiO₂ (Soot Stream) + 4HCl

Unstable Boundary Layer:
[ Nozzle Tip ] ──> Eddy Currents / Micro-Recirculation ──> Soot Trapping ──> Vitrified Glass Crust
1. The Physics Behind Soot Recirculation
An OVD torch relies on a precise velocity differential between its concentric gas rings:
-
Inner Core: Precursor vapor carrying SiCl₄ and argon carrier gas.
-
Intermediate Barrier: Inner shielding gas (typically Ar or N₂) isolating the raw precursor from active combustants.
-
Combustion Ring: High-velocity hydrogen (H₂) and oxygen (O₂) driving the thermal hydrolysis.
-
Outer Curtain: Shielding oxygen preventing ambient air ingress and controlling flame width.
Soot buildup occurs when the shielding gas velocity falls below the critical threshold required to push the reaction zone away from the metallic faceplate. This velocity deficit creates localized low-pressure eddy currents immediately adjacent to the chemical orifices.
Soot particles become trapped in these micro-vortices, reversing toward the nozzle face where surface temperature easily converts loose soot into bonded silica glass.
2. Microscopic Tooling Flaws That Trigger Early Clogging
While gas flow meters may display balanced mass flow readings, physical imperfections inside the burner nozzle channels frequently generate unmeasured flow resistance.
| Tooling Defect | Immediate Impact on Gas Stream | Operational Consequence |
| Micro-Burrs at Orifice Exit | Disrupts laminar flow; generates local turbulence | Particles nucleate directly on burr edges |
| Annular Eccentricity | Concentrates gas velocity to one side of the ring | Low-velocity zone on opposing side sucks soot inward |
| Internal Surface Roughness | Drag reduces boundary velocity along channel walls | Premature precursor mixing inside the nozzle body |
| Thermal Expansion Mismatch | Distorts orifice roundness during prolonged runs | Flame narrows; soot falls back onto nozzle rim |
Producing gas distribution nozzles with multi-axis CNC turn-mill machining ensures the inner chemical tubes and outer shielding channels remain concentric under single-clamping production. Eliminating tool chatter marks inside micro-channels maintains laminar boundary integrity, keeping the chemical reaction safely detached from the metal surface.
3. Cleaning Mistakes That Destroy Torch Orifices
When vitrified crust builds up, maintenance crews often inadvertently ruin the torch during reconditioning:
-
Mechanical Scraping with Steel Picks: Scraping off bonded silica using hardened metal tools inevitably nicks the orifice lip. A microscopic scratch of just a few microns on the discharge rim is enough to act as an anchor point for rapid soot accumulation in the subsequent run.
-
Aggressive Acid Soaks Without Neutralization: Submerging aluminum components in harsh chemical baths strips away the protective anodized layer and broadens the orifice margins, permanently altering gas exit velocities.
-
Compressed Air Purging from Front to Back: Blowing particulate back into the nozzle pushes loose soot deep into internal annular chambers, causing internal blockage that cannot be flushed during normal gas operation.
The Proper Maintenance Workflow:
-
Ultrasonic bath immersion utilizing a mild surfactant or tailored chelating agent to dissolve chloride residues without attacking base metals.
-
Controlled thermal expansion softening if glass crusting is severe, followed by non-marring polymer tools to lift the residue.
-
Cleanroom drying and optical magnification inspection to confirm zero edge burring or channel deformation before reinstallation.
4. Material Selection: Why Titanium Outlasts Aluminum
Standard 6000-series aerospace aluminum is cost-effective and machines easily, but its thermal threshold creates operational vulnerabilities in high-deposition core runs. Radiant heat causes aluminum nozzle rims to soften slightly, increasing surface reactivity and adhesion toward hot silica particles.
Upgrading core faceplate components to Grade 5 Titanium Alloy changes this dynamic:
-
Inert Surface Chemistry: Titanium spontaneously develops a dense, passive oxide barrier (TiO₂) that exhibits far less chemical affinity for molten silica soot than aluminum oxide.
-
Structural Rigidity Under Thermal Soak: Titanium retains its mechanical stiffness and channel geometry even when exposed to high radiant loads, preventing thermal warping of thin gas slit margins.
-
Resistance to Corrosive Acid Byproducts: Hydrochloric acid (HCl) generated at the flame front rapidly micro-pits aluminum channels, whereas titanium exhibits near-total immunity under standard deposition atmospheres.
Optimizing Your Deposition Lathe Reliability
Clogging is rarely just a “gas supply issue”—it is the mechanical interaction of alloy durability, internal channel micro-finish, and thermal management.
To eliminate premature vitrification on your production lines, transition critical high-wear stages to our Titanium OVD Burner Assemblies or stabilize end-stroke thermal transitions with an OVD Auxiliary Tail Burner & Oxygen Distribution Manifold.
Browse our comprehensive inventory of optical fiber equipment parts and burner spares, or submit your custom CAD drawings to our technical engineering team for make-to-print component support.
