
지식
VAD Cladding Burner Components: Key Questions Before Custom Machining
10월
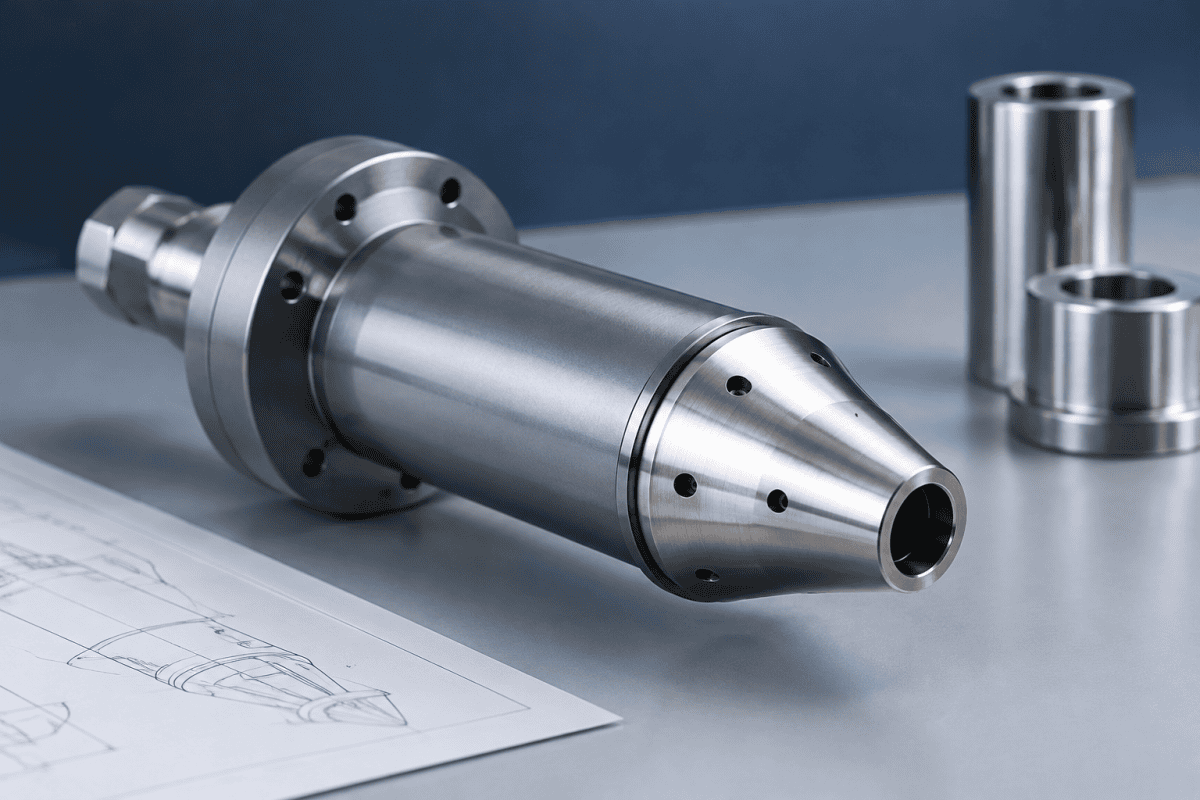
Specifying VAD cladding burner components for custom machining is a decision that locks in months of production behavior. The cladding burner sits in a demanding position in the VAD process: it deposits large volumes of silica soot onto a rotating seed rod, and its geometry and gas distribution directly influence deposition efficiency, preform diameter consistency, and the usable length of the final preform. Unlike an off-the-shelf replacement, a custom-machined VAD cladding burner must be defined by the process it serves, not just by the dimensions of the part it replaces. This article covers the key questions engineers and procurement teams should answer before releasing a drawing for custom deposition burner machining.
Why VAD Cladding Burner Components Are Not Interchangeable With Other Torches
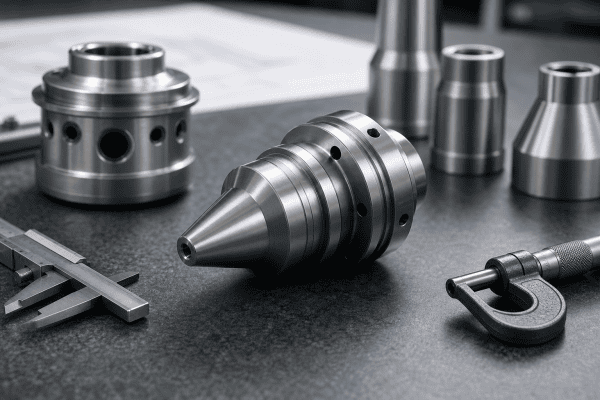
VAD (vapor axial deposition) builds a porous soot preform by depositing material axially onto a rotating target rod, with the cladding burner typically positioned to deliver a high-throughput soot stream over a large area. This is a different duty from an OVD burner, which builds layers on the outside surface of a bait rod, and it is very different from an MCVD torch, which heats the outside of a substrate tube to drive an in-tube reaction. The cladding stage in VAD usually accounts for the largest share of deposited volume, so small inefficiencies in the cladding burner are amplified across the whole preform.
Because of these differences, a burner that performs well in an OVD or MCVD position should not be assumed to perform well in a VAD cladding position. Gas channel counts, exit geometry, faceplate design, cooling provisions, and mounting interfaces all reflect the process they were designed for. Before custom machining, the first question is not “what dimensions do we copy?” but “what does this burner actually have to do in the VAD cladding stage?”
Industry reference material such as the Corning Glass Age resources on optical fiber development can help frame how torch design evolved alongside preform processes, which is useful context when reviewing internal legacy drawings.
Define the Process Requirements Before the Geometry
Machining a burner is fast compared to diagnosing why it does not perform. Getting the requirements right first reduces the risk of a second iteration. The following inputs are worth documenting before any drawing work begins.
Deposition rate and soot pattern
What deposition rate must the cladding burner sustain, and how uniform must the soot stream be across the target? A cladding burner that produces a narrow, high-velocity stream may build thickness quickly in one zone while leaving the edges under-deposited. A broader, more diffuse pattern improves coverage but can reduce capture efficiency. The nozzle array, orifice sizing, and channel spacing all follow from this decision, so it should be settled before geometry is fixed.
Gas channels and chemistry
How many separate gas and vapor channels does the burner require? VAD cladding burner components commonly handle fuel gas, oxygen or an oxidizer, and vaporized precursor delivered from a separate delivery system, plus possibly a shielding or purge channel. Each channel needs its own internal path, inlet fitting, and sealing arrangement. The number of channels affects the internal layout, wall thicknesses, and the machining sequence — and it is one of the most common sources of rework when it is not frozen early.
Mounting and alignment
How does the burner locate in the VAD lathe or deposition station? Angular alignment relative to the target rod, standoff distance, and repeatability of the mounting interface all influence where the soot actually lands. If the burner is removed and replaced during maintenance, the mounting design should allow it to return to the same position without re-alignment measurement. This is an interface question as much as a machining question.
Material Selection Is an Engineering Decision, Not a Default
Material choice for VAD cladding burner components depends on the function of the specific part: faceplate, nozzle insert, body, cooling jacket, or mounting flange. Each sees a different combination of temperature, thermal cycling, gas chemistry, and mechanical load.
Key factors to weigh include:
- Thermal exposure and cycling. The faceplate and nozzle tips are closest to the reaction zone and experience the steepest gradients. Materials with good thermal conductivity help move heat into the cooling circuit, while materials with low thermal expansion reduce distortion as the burner heats and cools between runs.
- Chemical environment. Precursor vapors, halide-containing species, and combustion products can attack certain alloys at elevated temperature. The material must be compatible with the actual chemistry the burner sees, not just with the gases listed on a general process sheet.
- Machinability and feature definition. Small orifices, shallow channels, and fine sealing surfaces demand a material that can hold tolerance without excessive tool wear or surface damage. Difficult-to-machine materials can drive cost and lead time more than the raw stock price suggests.
- Galvanic and sealing compatibility. Mixed materials in one assembly can create corrosion risks and differential expansion at joints. Seal and fitting materials must also suit the operating temperature and chemistry.
Aluminum, for example, suits some burner bodies and structural parts where weight and thermal conductivity matter, but its temperature limits make it unsuitable for the hottest internal surfaces. This is why material suitability should always be presented as a function of the component’s role rather than applied as a blanket choice across a burner. For a structured view of how material and geometry decisions interact in burner design, the guide to custom burner sourcing, materials, and reverse engineering is a useful reference for preform engineers.
For a side-by-side look at how channel layouts and exit geometries differ between process families, the comparison of OVD, VAD, and MCVD torch nozzles is a practical companion to the questions below.
Questions to Answer About the Existing Component
Most custom VAD torch parts projects start from an existing burner, either because it is worn, obsolete, or no longer supplied. Reverse engineering is a legitimate route, but it requires more than measuring a part.
What is the failure mode?
If the burner is being replaced because of a performance problem, that problem needs to be characterized. Faceplate soot buildup, distortion after thermal cycling, erosion at nozzle exits, and internal channel blockage each point to different corrective priorities. Copying a worn part without understanding its wear pattern risks reproducing the same failure. Articles on preventing soot clogging on burner faceplates and burner maintenance and lifespan discuss these mechanisms in more detail and can help frame inspection findings.
Is the drawing trustworthy?
Original drawings may be outdated, incomplete, or reflect a design revision that was never documented. Where possible, verify supplied dimensions against the physical part and against the process requirements. Discrepancies between the drawing, the measured part, and the intended function should be resolved before machining, not after.
Which features are functional and which are incidental?
Not every dimension on a worn part matters equally. Critical features typically include orifice diameters and spacing, channel cross-sections, faceplate flatness, sealing surfaces, and mounting datums. Cosmetic features, external contours, and non-functional radii can often be adjusted for manufacturability without affecting performance. Separating critical from non-critical dimensions gives the machine shop room to produce a robust part instead of an unnecessarily difficult one.
Inspection and Verification Points to Specify
When releasing VAD cladding burner components for machining, the inspection plan should match the features that affect deposition. Consider specifying:
- Orifice diameter and position tolerances, with the measurement method defined.
- Faceplate flatness and surface finish, since these affect flow uniformity at the exit.
- Channel-to-channel alignment and concentricity where gas streams must converge.
- Sealing surface finish and flatness at gas inlets and joints.
- Mounting datum verification, so the part locates correctly in the deposition station.
- Pressure or leak testing of internal channels before acceptance, using a procedure agreed with the supplier.
For multi-channel burners, the relationship between channels matters as much as each channel individually. If internal paths are not balanced, gas distribution can shift across the faceplate and alter the soot pattern. Specifying balance at the drawing stage is cheaper than correcting it on the lathe, and it belongs alongside the dimensional tolerances in the acceptance criteria.
Gas Channel Design Details That Drive Machining Cost
Beyond the number of channels, the internal geometry of each path has a direct effect on how the burner is manufactured and how it performs. VAD cladding burner components with long, small-diameter drilled passages are harder to clean and inspect than parts with milled channels and removable covers. Where the process allows, designing for access during cleaning can extend service life and reduce the risk of hidden blockage.
Channel transitions deserve particular attention. Abrupt steps, sharp internal corners, and mismatched cross-sections at joints create turbulence and dead zones where precursor can accumulate. Smooth transitions and generous radii are usually easier to machine consistently and behave more predictably in service. If a legacy drawing shows a sharp transition that is difficult to reproduce, it is worth asking whether the feature is functional or simply an artifact of the original manufacturing method.
Sealing strategy is another decision point. Metal-to-metal seals, elastomer seals, and gasketed joints each have different temperature limits and reusability characteristics. For VAD cladding burner components that see repeated thermal cycling, the seal type affects both maintenance intervals and the risk of leakage at high temperature. This choice should be made alongside the material selection, not after the drawing is released.
Sourcing and Communication Checklist
A complete inquiry package shortens quoting and reduces the chance of a mismatched part. Before contacting a supplier, assemble the following:
- Component function and position in the VAD cladding stage.
- Available drawings, models, or the physical sample part.
- Measured critical dimensions with tolerances, noting which are functional.
- Material requirements by component area, with operating conditions noted.
- Gas channel list, inlet fitting types, and connection details.
- Mounting interface dimensions and alignment requirements.
- Known failure history and any performance targets for the replacement.
- Quantity and any documentation or traceability requirements.
If some of these inputs are unavailable, say so. A supplier who understands that a dimension is estimated rather than verified can flag risk areas and propose a verification step. The optical fiber equipment sourcing FAQ addresses several common questions about drawings, samples, and non-standard parts.
Matching the Machining Approach to the Burner
Custom deposition burner machining is not a single operation. It typically combines turning for bodies and nozzles, milling for channels and mounting features, drilling or EDM for small orifices, and precision finishing for sealing and flow surfaces. The sequence matters: internal channels usually need to be formed and cleaned before final assembly, and heat treatment or stress relief, where required, must be planned so it does not distort finished tolerances.
Where multi-channel bodies are involved, the way those channels are stacked, sealed, and machined has its own set of constraints. A review of the approach to machining multi-channel burner bodies can help clarify what is practical before the design is frozen.
For complex or obsolete burners, a supplier with experience in drawing-based production and sample-based reverse engineering can propose a manufacturable geometry rather than an exact but impractical copy. Reviewing the range of burner head replacement and gas connection checks is a reasonable step once the requirements above are documented.
It is also worth agreeing on how replacement VAD cladding burner components will be installed. Dimensional checks at the mounting interface, nozzle-to-faceplate fit, and gas inlet orientation should be part of the handover so the part can be brought into service without a second round of machining.
How Many Spares Should You Hold?
Spare-part strategy affects both uptime and the economics of custom machining. VAD cladding burner components that wear predictably can be managed with a scheduled replacement interval, but components that fail unpredictably may justify holding a complete spare burner rather than individual parts. The right answer depends on lead time, the cost of a deposition interruption, and whether the failure mode can be detected during routine inspection.
For custom parts, it is worth discussing whether a small first batch and a follow-up production run is more practical than a single large order. A first article can be inspected and run in production before committing to a full quantity, which reduces the risk of discovering a dimensional or performance issue after a large lot has been completed. This approach also gives the supplier feedback that can be applied to later parts.
Documentation should be part of the spare-parts plan as well. Keeping the final as-built drawing, inspection records, and material certificates with the spare parts makes it much easier to reorder VAD cladding burner components years later, even if the original supplier contact has changed. Where a part is reverse engineered, the measurement report and the agreed specification become the reference document for future orders.
자주 묻는 질문
Can VAD cladding burner components be copied directly from a worn sample?
Measurement is a starting point, not a specification. Wear, distortion, and deposits can make the sample differ from the original design. Critical features should be measured on clean, stable surfaces and reconciled with the process requirements and any available drawings before machining.
Should all VAD burner components use the same material?
No. Faceplates, nozzle inserts, bodies, and cooling components see different temperatures, chemistries, and loads. Material should be selected per component function, and where a mixed-material assembly is used, expansion and galvanic compatibility at joints should be reviewed.
What is the most common cause of a poor first-iteration burner?
Undefined requirements. When channel count, deposition pattern, mounting alignment, or critical tolerances are left ambiguous, the shop must guess, and the resulting part may not match the process. Freezing these inputs before machining is the most effective way to avoid rework.
Do VAD cladding burner components need leak or flow testing?
For burners with internal gas channels, some form of pressure or leak verification before acceptance is generally advisable. The specific method, pressure, and acceptance criteria should be agreed with the supplier and based on the equipment documentation and the site’s safety procedures.
다음 단계
The most useful preparation for a VAD cladding burner project is a clear, written statement of requirements: what the burner must do, which dimensions are functional, which materials suit each area, and how the part will be inspected. Teams that document these points before issuing a drawing usually find that VAD cladding burner components are easier to quote, faster to machine, and more predictable in service.
If you have drawings, a worn sample, critical dimensions, or operating conditions to share, contact our team to discuss the component and request a quotation.
